


 English
 Español


DLP Resin 3D Printing Service Manufacturer
Zhejiang Jiaheng Intelligent Equipment Manufacturing Co., Ltd. is a China DLP resin 3D printing service manufacturer and OEM/ODM factory. Our DLP Resin 3D Printing Service uses full-layer exposure to build resin parts with fast build speeds and extremely fine texture detail, and it sits inside our wider one-stop platform covering 3D printing, CNC machining, vacuum casting and surface finishing.
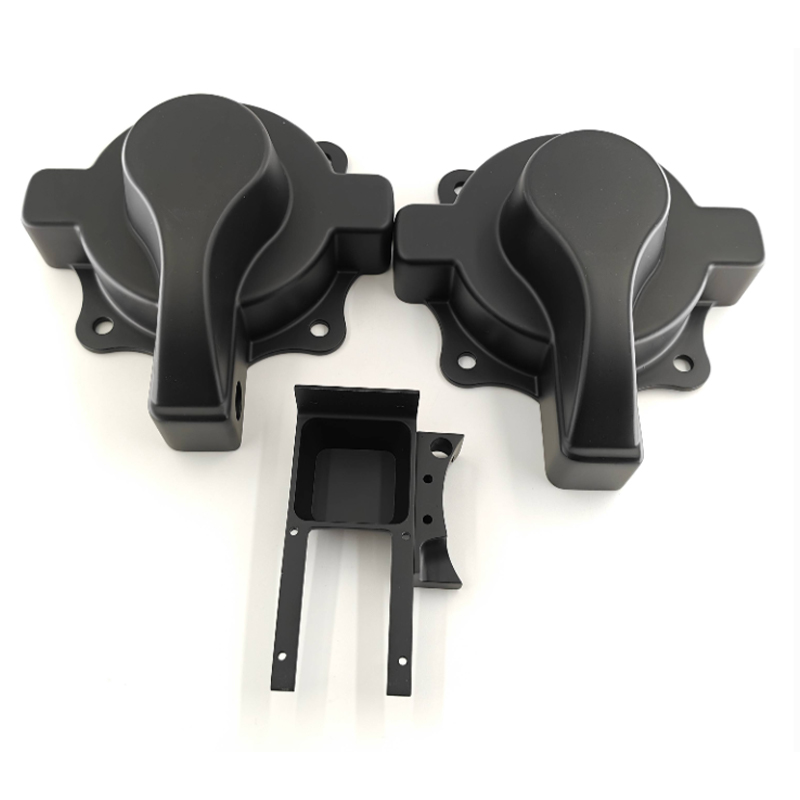
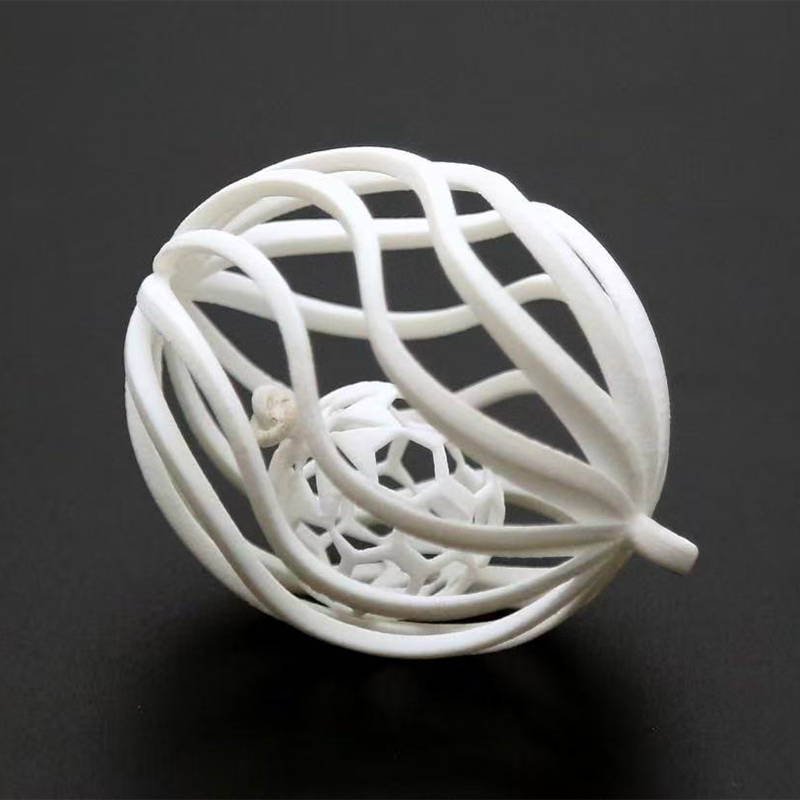
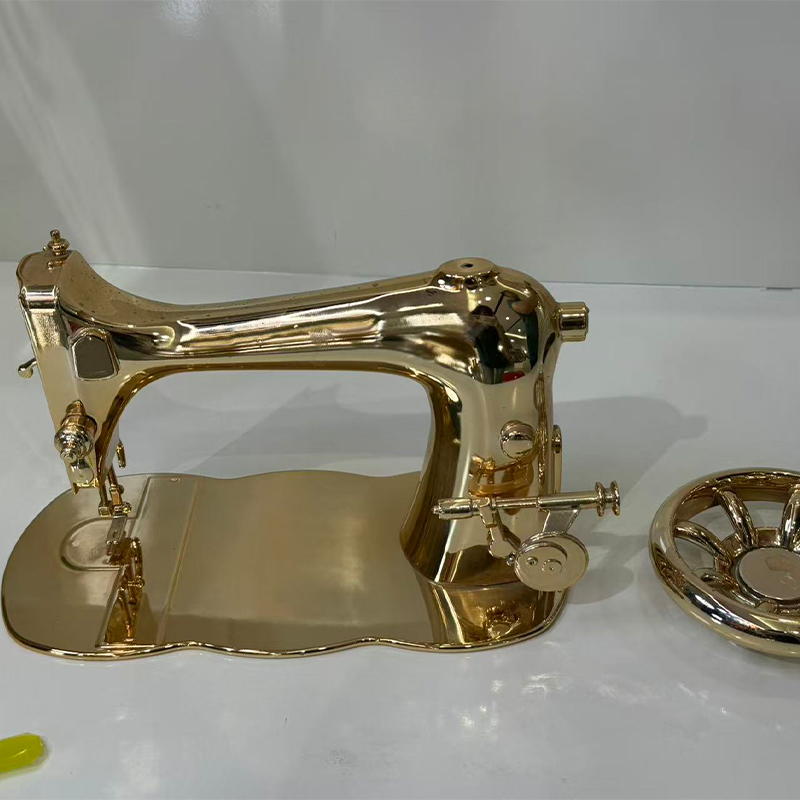
We produce small, complex, high-detail resin components for jewelry, figurines, dental models and comparable precision parts, and we support prototype samples through to small-batch and contract production from our Jiaxing production base.
How DLP Resin Printing Works and Where It Fits
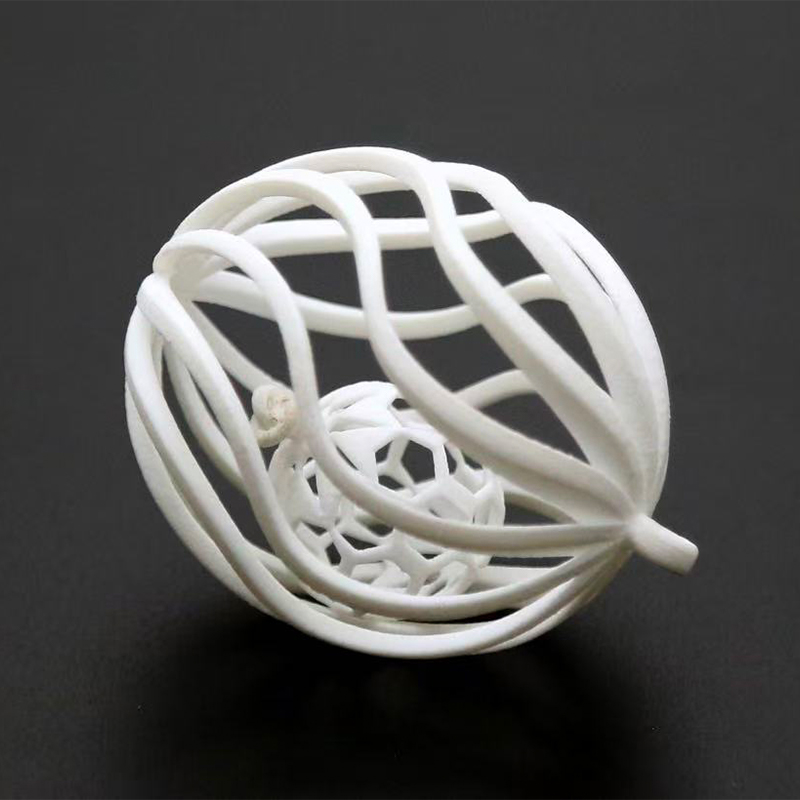
Digital light processing projects a full layer image onto the resin surface at once, so each layer cures in a single exposure rather than being traced point by point. That is the source of two practical advantages: faster build speed than point-by-point scanning SLA, and high precision on small, intricate geometry.
Because the projected pixel grid defines the smallest addressable feature, DLP suits parts whose value sits in fine surface texture, sharp edges and small repeating detail. Where a part is large and thin-walled rather than fine-detailed, our SLA Resin 3D Printing Service is often the better route; where the requirement is functional nylon or metal, we move the job to SLS Nylon 3D Printing Service or SLM Metal 3D Printing Service.
Process Advantages We Build Around
- Faster build speed than point-by-point scanning SLA process.
- Higher precision, ideal for small and complex structures.
- Delicate surface texture with excellent reproduction quality.
- Full-layer exposure keeps layer-to-layer consistency across a build plate.
Application Fit by Part Type
DLP resin output is chosen when surface detail and dimensional fidelity on small parts matter more than mechanical load. The table below maps typical part families to the way we configure the job.
| Part Family | Why DLP Fits | Typical Configuration |
|---|---|---|
| Jewelry masters and patterns | Fine texture, sharp prongs and filigree | High-detail resin, small build plate, casting-ready orientation |
| Figurines and collectibles | Surface reproduction on sculpted detail | Multi-part splitting, support planning, post-cure and finishing |
| Dental and medical models | Accurate small geometry and smooth surfaces | Model resin, tight layer control, dimensional verification |
| Small precision components | Complex features that would need multiple machining setups | Resin selection by function, then CNC or finishing if required |
| Casting patterns | Clean burnout behaviour and fine as-printed texture | Red Wax Resin 3D Printing Service |
Red Wax Resin: Our Dedicated Casting Material
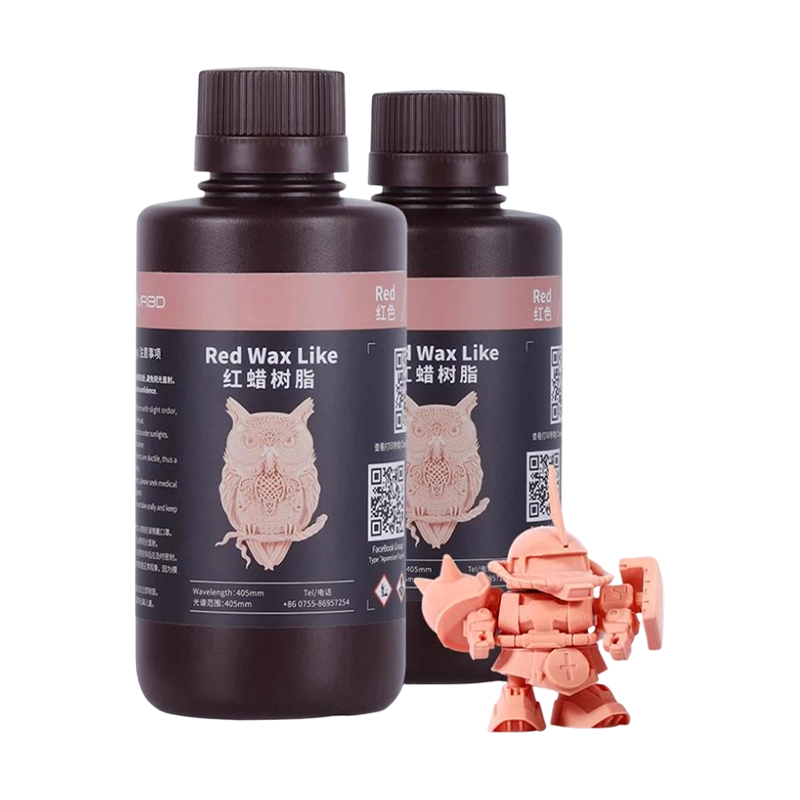
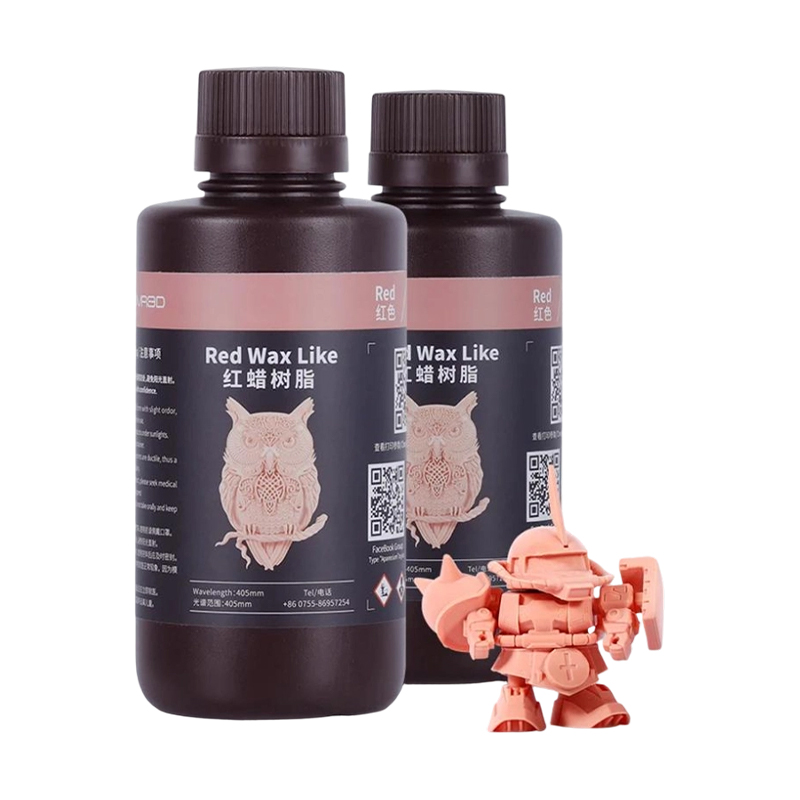
Red Wax Resin is the dedicated casting material for our DLP resin service. It is a high-precision, fine-texture-detail resin developed for patterns that go straight into investment casting, achieving extremely fine surface texture so the cast surface starts from a clean pattern.
We pair it with the same DLP platform used for our standard detail resin, so a jewelry or dental pattern and its functional counterpart can be produced on one process route with consistent build behaviour.
Specifications That Drive the Build
DLP output is defined by a small set of variables. We confirm these against the drawing before a build is scheduled, because they set the achievable detail, the orientation and the finishing route.
- Layer thickness — the primary trade-off between build time and surface smoothness on curved and sloped faces.
- XY pixel resolution — sets the smallest addressable feature and the sharpness of fine edges.
- Build envelope — determines whether a part prints in one piece or is split and assembled.
- Orientation and supports — controls witness marks, flatness and where support removal is acceptable.
- Resin grade — detail resin, casting resin such as Red Wax, or a functional grade matched to the end use.
- Wall thickness and drainage — governs hollowing, resin evacuation and internal cure.
- Post-processing — washing, post-cure, support removal, sanding and polishing to the required finish.
From Print to Finished Part
A DLP build is only one step in the route to a usable part. We plan the downstream operations at quotation stage so the printed geometry already accounts for them.
Typical route: file review and orientation → DLP build → support removal → washing and post-cure → dimensional and appearance inspection → finishing or downstream process.
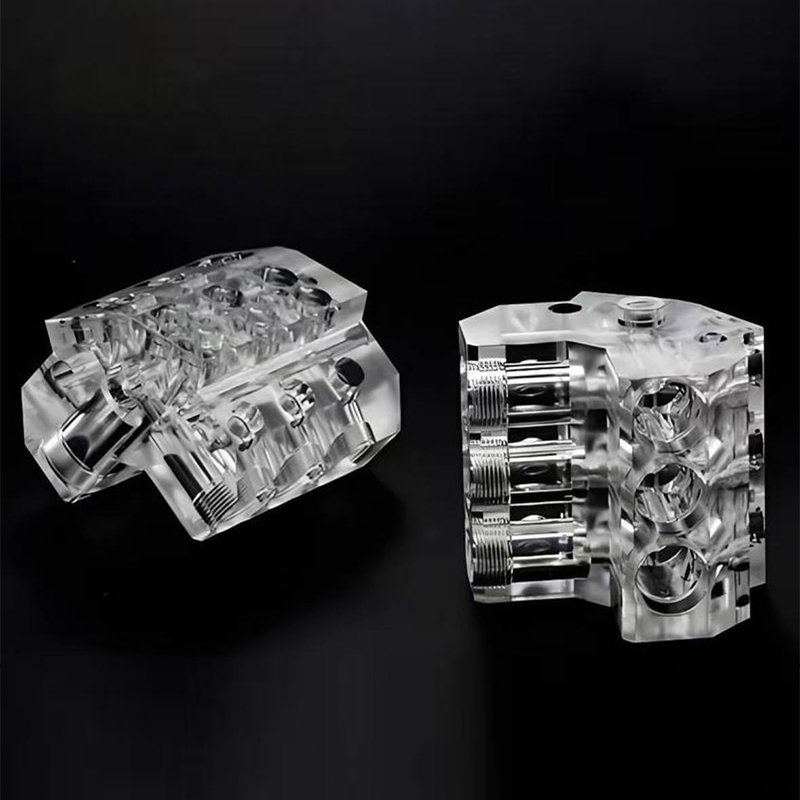
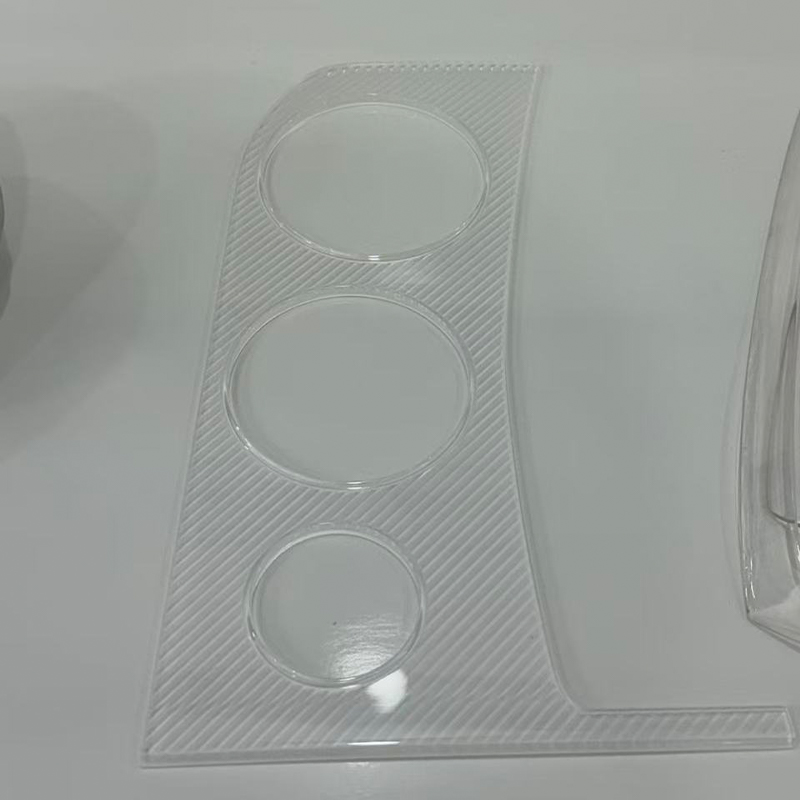
Downstream options include Painting & Coating (Matte / Glossy Finish), Grinding, Polishing & Sandblasting, and Transparent Parts (Semi-Transparent / Fully Transparent) where clarity is required.
Quality Control and Confidentiality
We implement full-process quality inspection covering raw material incoming check, semi-finished product testing and finished product dimension verification. Every customized workpiece is inspected against dimensional tolerance and appearance standards so precision and quality stay consistent across prototype and batch production.
- Raw material inspection — resins are checked before storage to cut quality risk at source.
- In-process sampling — periodic sampling during production stabilizes machining precision.
- Final shipment check — finished parts receive comprehensive inspection before delivery.
- Project zoning — independent closed workshops separate customer projects to avoid cross-data leakage.
- Staff NDA and isolated network — non-disclosure agreements and an internal isolated network protect drawings and models.
Where DLP Sits in Our Range
DLP is one process in a connected manufacturing platform. When a project needs more than resin detail, we move it across processes without changing supplier or re-explaining the part.
| Process | Best Fit |
|---|---|
| DLP resin printing | Small, complex, high-detail parts; jewelry, figurines, dental models; casting patterns |
| SLA resin printing | Larger resin parts, smooth surfaces, transparent and semi-transparent work |
| SLS nylon printing | Functional nylon parts, living hinges, snap fits, no support marks |
| SLM metal printing | Metal components in tool steel, titanium, aluminium and stainless steel |
| CNC machining | Tight-tolerance functional parts and post-print machining |
| Vacuum casting | Low-cost, high-precision small-batch replication from a printed or machined master |
Information We Use to Configure Your Solution
Our proposal is based on the working point, material and production target. The following inputs let us confirm process route, orientation, finishing and batch plan without back-and-forth.
- 3D model in STEP, STL or the native CAD format, plus 2D drawing where tolerances are called out.
- Part function and end use — display model, casting pattern, fit-check part or functional component.
- Critical dimensions, tolerances and the surfaces that must not carry support marks.
- Required surface finish and colour, including any transparency requirement.
- Quantity per revision and expected total volume, so we can plan build nesting and batch runs.
- Any downstream process the part must survive, such as casting, coating or assembly.
- Delivery destination and packaging expectations for the shipment scope.
Frequently Asked Questions
What makes DLP different from SLA for my part?
DLP exposes a whole layer at once, so it builds faster than point-by-point scanning SLA and holds high precision on small, complex structures. We recommend DLP when fine texture detail on small parts is the priority, and SLA when the part is larger or needs a different surface and material profile.
Which resin should be used for a casting pattern?
Red Wax Resin is our dedicated casting material. It is a high-precision, fine-texture-detail resin that produces clean patterns for investment casting, and it runs on the same DLP platform as our standard detail resin.
Can you produce both a prototype and a small batch?
Yes. We accept custom orders of all batch sizes. A printed master can also be replicated through vacuum casting for low-cost, high-precision small-batch production, so the same geometry moves from one-off sample to a repeatable batch.
How is dimensional quality verified before shipment?
We run full-process inspection: raw material incoming check, in-process sampling during production, and finished product dimension verification against the drawing tolerances and appearance standards. Only parts that pass the final check are packed for delivery.
How are drawings and models protected?
Customer projects are separated in independent closed workshops, all staff sign non-disclosure agreements, and drawing files are held on an internal isolated network that prevents unauthorized external transmission.
What finishing can follow a DLP build?
After support removal, washing and post-cure, parts can be sanded and polished, sandblasted, painted in matte or glossy finishes, or treated for transparent and semi-transparent appearance. We plan the finishing route at quotation stage so the printed geometry already accounts for it.


